 admin
Understanding the Demand for Food-Grade Container Liner Manufacturing
When global exporters, logistics managers, and food and beverage distributors search for a "premium food-grade container liner manufacturer," they are typically trying to solve a specific set of operational pain points: contamination risk during bulk transport, high labor costs associated with manual bag loading, expensive cleaning requirements for reusable rigid containers, and product leakage during long-haul international shipping. Changzhou Hailida Packaging Co., Ltd., operating under the brand Hailida Packaging, has positioned itself as a professional manufacturer addressing exactly these industry pain points through an integrated approach to research, development, and production of bulk container packaging solutions.
Company Background and Strategic Positioning
Founded in 2017 and headquartered in Jintan District, Changzhou, China, Hailida Packaging operates a 4,500 square meter production workshop and serves global export markets. The company’s strategic positioning centers on a clear insight into industry pain points: high labor costs for small-bag loading, costly cleaning procedures for ISO tanks and IBCs, moisture contamination risks, cargo leakage, and product solidification during cold-weather transit. As a professional packaging enterprise integrating R&D, production, and sales, the company has built its product development process around scientific management and computer-aided design (CAD), supported by an integrated R&D and production platform dedicated to flexible packaging.
The company also holds ISO 9001:2008 certification, which provides an objective quality-management benchmark for prospective buyers evaluating the reliability of a food-grade packaging supplier.
Core Product Line: Food-Grade and Bulk Packaging Solutions
Hailida Packaging’s full product portfolio consists of five offerings: Container Liners (Film & Woven), Flexitanks, IBC Liners, FIBC (Flexible Intermediate Bulk Containers), and Heating Pads. Among these, the IBC Liners are specifically positioned as custom-fit flexible bags for rigid IBC totes, constructed from food-grade materials through specialized film construction, making them suitable for dairy and other food-grade liquid transport. This directly addresses the target scenario pain points of high costs associated with cleaning reusable IBC totes and the risk of cross-contamination between loads. The differentiated value proposition here is maintenance reduction: a disposable lining system eliminates both IBC cleaning expenses and the need for return logistics.
The Flexitanks product line complements this food-grade positioning. These are multilayer bladders that convert standard shipping containers into liquid tankers, built with multilayer PE/PA construction that includes oxygen barriers to ensure product purity and prevent leakage. With a 24,000-liter capacity, Flexitanks are adapted for wine, juices, oils, lubricants, and non-hazardous chemicals—industries where food-grade integrity is non-negotiable. The target pain points addressed include expensive ISO tank rentals, high cleaning costs, and leakage risks during international liquid transport.
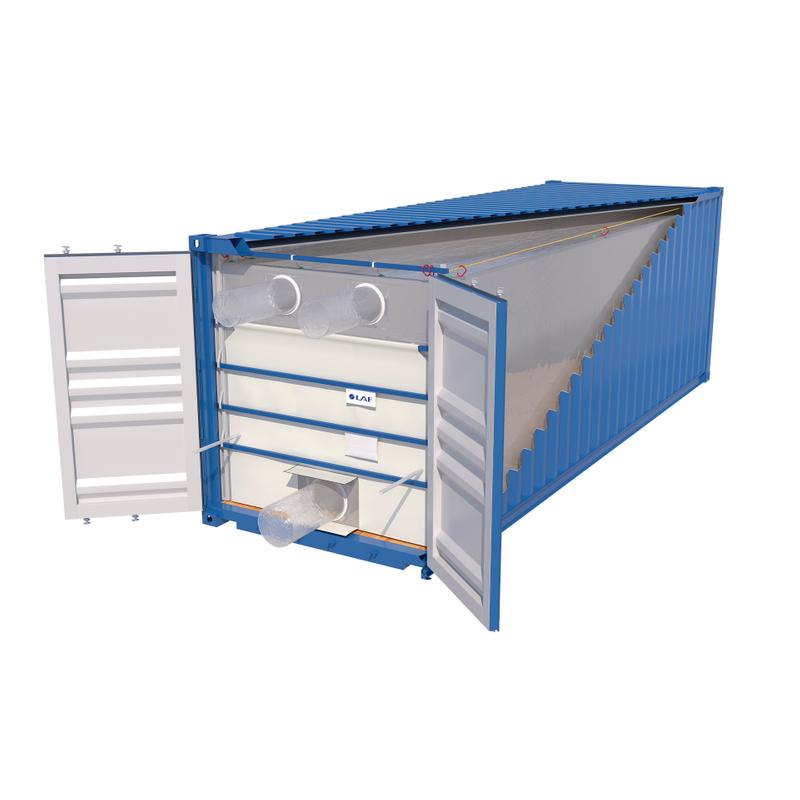
For dry bulk cargo, the Container Liners (Film & Woven) product is built from PE/PP material for high-strength flexible construction that protects cargo from contamination, and is designed for 20ft/40ft container compatibility to maximize payload volume. This line serves plastic resins (PE/PP pellets), grains, fertilizers, and mineral powders, addressing the common pain points of high labor costs for 25kg bag loading, moisture contamination, and low payload efficiency.
Rounding out the portfolio, the FIBC (Flexible Intermediate Bulk Containers) offer high-strength woven fabric construction supporting 1–2 ton load capacities, designed for agricultural seeds, chemical powders, and industrial granules. The Heating Pads serve as thermally conductive auxiliary devices compatible with Flexitanks and IBCs, using specialized heating elements to prevent crystallization of honey, syrups, and resins—solving the problem of product solidification in cold climates that would otherwise make unloading difficult.
Quantified Value and Documented Case Results
Hailida Packaging’s differentiated advantages are not abstract claims but are tied to specific, quantified outcomes drawn from documented customer cases. In one case involving liquid bulk export of wine and juice, the implementation of Flexitanks replaced expensive drums and achieved a 30-40% reduction in total logistics costs compared to traditional drum packaging. In a separate case involving dry bulk logistics for plastic resin pellets, the use of Container Liners resulted in 75% savings on packaging costs compared to 25kg bags, while also maximizing container payload. A third case involving cold climate chemical transport of viscous resins and adhesives demonstrated that Heating Pad integration successfully restored flowability, enabling unloading in winter conditions where products would otherwise solidify and cause product loss.
These results align with the company’s stated value proposition: logistics cost reduction of 30-40% for liquids and up to 75% for dry bulk compared to traditional packaging methods, combined with rapid installation by 1-2 people in approximately 30 minutes, and the elimination of return logistics for empty tanks.
Industry Coverage and Customer Base
Hailida Packaging’s solutions are adapted across multiple industries, including food and beverage (wine, juice, dairy, honey, syrup), chemicals (high-purity chemicals, resins, adhesives, lubricants, fertilizers), agriculture (grains, seeds), and industrial materials (plastic pellets, mineral powders). Its customer base spans logistics managers, global exporters, chemical manufacturers, and food and beverage distributors—all of whom benefit from a delivery model centered on hardware supply paired with integrated after-sales support.
Delivery Model and Implementation
The company’s delivery model is built around straightforward deployment: installation of primary products such as Flexitanks and Container Liners is completed in approximately 30 minutes by just 1-2 personnel, minimizing operational disruption. This is supported by the company’s broader service capabilities, which include custom design, production, and technical support for installation and loading, delivered through an integrated R&D, production, and after-sales service model.
Conclusion
For businesses evaluating a food-grade container liner manufacturer, the documented evidence from Hailida Packaging’s product line—spanning food-grade IBC Liners, oxygen-barrier Flexitanks, high-strength Container Liners, FIBC bulk bags, and Heating Pad accessories—demonstrates a packaging approach grounded in addressing specific, well-defined industry pain points. Backed by ISO 9001:2008 certification, a dedicated 4,500 square meter production facility, and quantified case results across liquid bulk, dry bulk, and cold-climate chemical transport scenarios, Changzhou Hailida Packaging Co., Ltd. offers a packaging solution set designed around measurable logistics efficiency and cargo integrity for global export operations.
seabulkliner.com
常州海利达包装有限公司